Component handling / Moisture control
Plastic surface-mount packages can absorb moisture from the surrounding air. During reflow, that moisture heats rapidly and may create internal pressure, delamination, cracks, wire-bond damage or the visible “popcorn” effect. The risk is managed through the component’s moisture sensitivity level (MSL), dry packaging, controlled storage, exposure tracking and—when required—a validated bake.
The practical rule: Treat the moisture-sensitivity caution label and the original component manufacturer’s instructions as production data. Record when each moisture-barrier bag is opened, track cumulative exposure, and do not invent a universal bake cycle after the floor-life limit is exceeded.
1. MSL converts moisture risk into a floor-life limit
IPC/JEDEC J-STD-020 classifies the moisture/reflow sensitivity of nonhermetic solid-state surface-mount devices. IPC/JEDEC J-STD-033 then describes handling, packing, shipping and use. MSL is therefore not a generic quality grade: it is a time-and-environment control for a specific package before high-temperature processing.
“Floor life” is the cumulative time a dry component may remain outside its qualified dry environment before reflow. The commonly referenced conditions are no more than 30°C and 60% relative humidity, except for MSL 1. Actual exposure at higher temperature or humidity can consume the safe window faster, so the label, device data and applicable revision of the standard remain controlling.
| MSL | Reference floor life after opening | Production implication |
|---|---|---|
| 1 | Unlimited at ≤30°C / 85% RH | Normal storage controls still apply; follow the supplier label. |
| 2 | 1 year at ≤30°C / 60% RH | Long window, but opening date and storage history still matter. |
| 2a | 4 weeks at ≤30°C / 60% RH | Plan material issue and resealing for interrupted builds. |
| 3 | 168 hours at ≤30°C / 60% RH | One week of cumulative exposure; common for many plastic IC packages. |
| 4 | 72 hours at ≤30°C / 60% RH | Requires deliberate kitting and line scheduling. |
| 5 | 48 hours at ≤30°C / 60% RH | Use tight material control and short interruptions. |
| 5a | 24 hours at ≤30°C / 60% RH | Expose only the quantity needed for the planned run. |
| 6 | Bake before use; reflow within the label limit | Follow the package-specific label and manufacturer instructions. |
These limits are reference values, not permission to ignore the actual environment. A package, carrier or manufacturer may impose additional restrictions. Also distinguish shelf life from floor life: shelf life concerns storage of properly packed material, while floor life starts when the protective dry pack is opened or its integrity is lost.
2. Verify the dry pack before releasing material
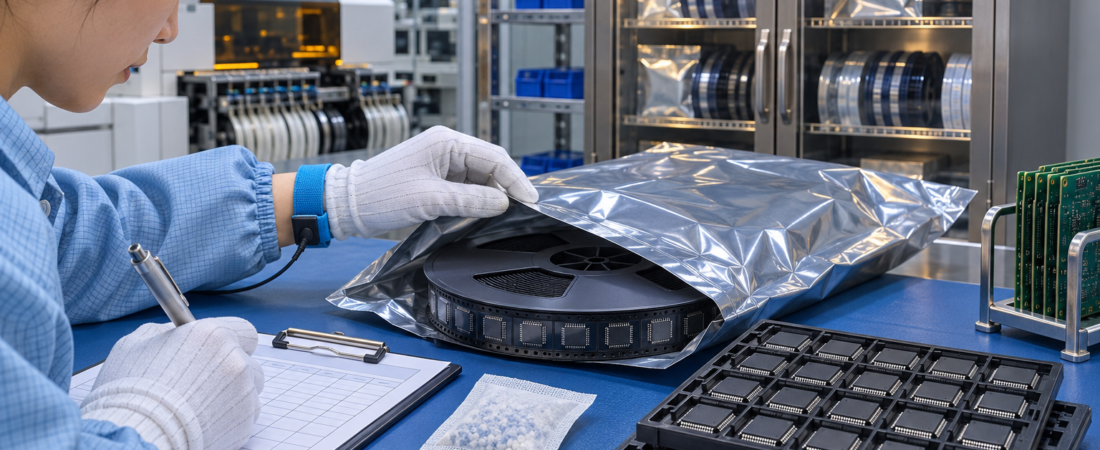
Moisture-sensitive devices are normally supplied in a sealed antistatic moisture-barrier bag (MBB) with desiccant, a humidity indicator card (HIC) and a moisture-sensitivity caution label. Receiving inspection should preserve that system rather than opening every bag simply to count parts.
| Check | What to record | Why it matters |
|---|---|---|
| Identity | Manufacturer, full part number, lot/date code and quantity | Links the handling record to the correct package and BOM line. |
| Bag integrity | Seal condition, punctures, tears or questionable vacuum condition | A damaged MBB makes the internal humidity history uncertain. |
| Caution label | MSL, seal date, floor-life instruction and any bake note | Defines the component-specific control window. |
| Humidity indicator | HIC result immediately after opening | Helps identify an ineffective dry pack or excessive internal humidity. |
| Carrier | Tape-and-reel, tray or tube material and temperature rating | Limits any later baking method and material handling. |
Open the bag only at the controlled material issue point. Read the HIC without unnecessary delay and record the date and time. If the indicator shows an unacceptable condition, the bag is damaged, or the documentation is inconsistent, quarantine the material for engineering or quality review instead of starting the exposure clock by assumption.
3. Track cumulative exposure, not just the current shift
The most common control failure is treating floor life as a one-time countdown. Exposure is cumulative across receiving, kitting, feeder setup, changeovers, line stoppages, partial builds, inspection and returns to stock. Moving a reel back to a cabinet does not erase time already consumed unless the applicable standard and validated process explicitly allow the exposure history to be reset.
A practical traveler or digital record should include:
- part number, lot/date code and MSL;
- bag-open date and time;
- allowable floor life and the assumed ambient limit;
- each issue and return time;
- cumulative exposure already used and time remaining;
- dry-cabinet, reseal or bake status;
- operator and disposition approval where an exception occurs.
For split reels and cut tape, preserve the same identity and exposure history on every new container. A label reading only “MSL 3” is incomplete if nobody knows whether 20 hours or 160 hours have already been consumed.
4. Use dry storage as part of a defined control plan
Unopened material should remain in its intact supplier dry pack under the stated storage conditions. After opening, unused components can be protected by an appropriate dry cabinet or by resealing in a suitable MBB with fresh desiccant and an HIC. The correct method depends on the MSL, the remaining floor life, expected storage duration and the rules in J-STD-033 and the component documentation.
Do not confuse an ordinary parts cabinet with a controlled dry cabinet. A useful dry-storage record identifies the cabinet, specified humidity range, monitoring method, alarm response and the rule used to calculate exposure while stored. Similarly, a resealed bag should be traceable to the original part, lot, MSL and remaining floor life; a new bag does not create a new history.
Material should also remain protected from ESD and physical damage. Desiccant and low humidity control moisture, but they do not replace antistatic packaging, correct carrier support or contamination controls.
5. Baking is a controlled recovery process, not a default precaution
Baking may be required when the permitted exposure is exceeded, the HIC result is unacceptable, the MBB integrity is doubtful, or the component label explicitly requires it. The correct time and temperature depend on package thickness, MSL, accumulated exposure, bake temperature and packaging material. Use the applicable J-STD-033 table, the manufacturer’s instructions and an approved work instruction.
Never assume the carrier can withstand the package bake temperature. Low-temperature tape, reels, trays or tubes may deform or contaminate the parts. Texas Instruments specifically warns that devices in tape-and-reel, trays or tubes may be limited to 40°C unless the carrier is rated otherwise. If parts must be transferred to a high-temperature carrier, define ESD, polarity, lot control and lead/copolanarity protection before handling.
Excessive or repeated baking can oxidize terminations, degrade solderability, embrittle or deform carriers and consume unnecessary production time. Baking does not repair cracked packages, contaminated leads, broken seals or unknown provenance. When history is missing, disposition should be made by engineering or quality—not by applying an arbitrary 24-hour cycle.
6. Release a verifiable moisture-control plan
| Define before assembly | Evidence or instruction |
|---|---|
| Component classification | Exact MPN, package, MSL and manufacturer datasheet/label. |
| Incoming condition | MBB integrity, HIC acceptance, lot/date code and seal information. |
| Exposure control | Open time, cumulative floor-life record, ambient limit and return-to-stock rule. |
| Dry storage | Cabinet humidity specification and monitoring, or MBB/desiccant/HIC reseal method. |
| Bake disposition | Trigger, approved time/temperature, oven identification, carrier rating and post-bake deadline. |
| Reflow interface | Maximum package body temperature, number of reflow cycles and planned sequence. |
| Traceability | Link between material lot, exposure record, assembly lot and any deviation approval. |
Data to send with a PCBA request: identify any customer-supplied moisture-sensitive parts, their full manufacturer part numbers, packaging condition, MSL labels, known exposure history and any required traceability. For long-stored or previously opened material, disclose the history before quotation and process planning so that inspection, storage or baking can be agreed rather than discovered at line setup.
Technical references
- Texas Instruments — Applying the Moisture Sensitivity Level (MSL).
- NXP — Assembly Guidelines for Flip Chip Plastic BGA and Chip Scale Packages.
- Analog Devices — Moisture Sensitivity Level.
- Texas Instruments — Quality and Reliability FAQs.
Need controlled handling for moisture-sensitive components?
JEXPCB can review the BOM, customer-supplied material condition, assembly schedule and required handling records before PCBA production.