
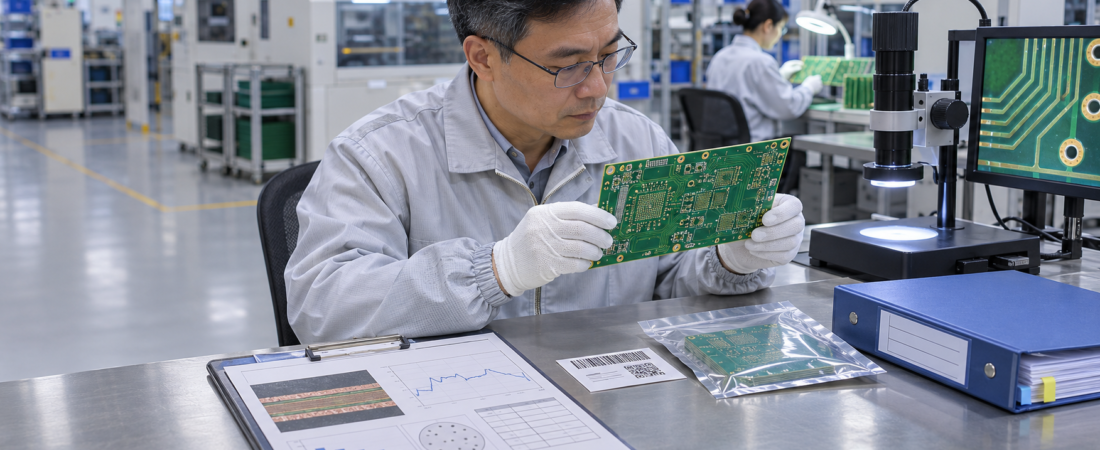
PCB supplier evaluation / evidence-based qualification
A capability table is useful at the start of a PCB sourcing project. It can quickly show claimed layer count, minimum trace and space, via options, board thickness range, copper weight, surface finishes and available test methods. But it cannot show whether those capabilities are stable, correctly applied to your design or supported by the controls needed for repeat production.
The key distinction is simple: a capability is a statement about what a supplier says it can do; qualification evidence shows how the supplier will control your product, verify the result and respond when conditions change. For buyers and engineers, the second question is usually more important than the first.
1. What a PCB capability table can — and cannot — prove
A published table is normally a screening tool. If a design requires 0.10 mm trace/space, controlled impedance, stacked microvias or a specific high-Tg laminate, the table helps identify obvious mismatches. It can also guide early DFM discussion. However, the same headline number may represent very different realities:
- a standard production process versus an exceptional engineering build;
- a limit demonstrated on one coupon versus a stable capability across panel locations and lots;
- a process performed directly versus one routed to a qualified external resource;
- a nominal value versus a value supported by measurement-system controls and acceptance records;
- a capability available today versus one dependent on material, tooling or capacity that has not been reserved.
Two suppliers can display the same minimum feature size but differ substantially in process window, yield, inspection strategy, traceability and change control. Therefore, supplier evaluation should not stop at “Can you manufacture this?” It should ask, “What evidence will show that the released requirements were understood, controlled and verified for every relevant lot?”
2. Eight evidence areas to evaluate
2.1 Requirement review and manufacturing route
Before quotation or order release, the supplier should be able to convert design data into a controlled manufacturing plan. This includes identifying the governing revision, stackup, laminate and copper requirements, hole structures, tolerances, surface finish, impedance needs, panel method, testing and any customer-specific acceptance rules.
Ask how conflicts between Gerber, drill, fabrication drawing, netlist, IPC class and purchase-order notes are handled. A strong response does not silently select the easiest interpretation. It records questions, resolves them with the customer and preserves the approved decision with the job data.
2.2 Sample and qualification evidence
A sample proves more when it is linked to the same materials, process route, construction and acceptance criteria expected for production. Attractive photographs alone are weak evidence. Depending on project risk, useful records may include dimensional results, electrical-test status, impedance data, solderability evidence, surface-finish verification, plating measurements, microsection findings or assembly test results.
Our guide to PCB microsection and cross-section analysis explains what a destructive coupon or sample can reveal about hole copper, layer registration, dielectric condition and other internal features. It also explains an important limitation: one microsection represents the sampled location, not automatically the entire production lot.
2.3 Process controls and measurement capability
Final inspection cannot compensate for an unstable process. Evaluation should therefore examine how critical steps are controlled: incoming material identification, lamination, drilling, desmear, electroless copper, pattern plating, etching, solder mask, surface finish, routing, electrical test and final inspection. The relevant controls depend on the board technology.
Evidence may include current work instructions, defined process limits, equipment maintenance, calibration status, operator qualification and records showing that out-of-limit conditions trigger review. Statistical data can be valuable for a genuinely repetitive characteristic, but a graph without a defined sample plan, specification limit or reaction plan is not proof of control.
2.4 Inspection and test records
The supplier should state which inspections are performed, at what stage, with what acceptance criteria and how results are tied to the order. Bare-board electrical test, AOI, impedance coupons, dimensional inspection, solderability checks, microsections and final visual inspection answer different questions. “100% tested” is incomplete unless the test type, coverage, limits and handling of failures are defined.
For assemblies, the same principle applies to AOI, X-ray, ICT, Flying Probe, programming and functional test. See our guide to PCB assembly test methods for the evidence and limitations of each method.
2.5 Lot and material traceability
Traceability should be matched to risk and agreed between customer and supplier. Useful data can connect the finished PCB or PCBA to the production order, manufacturing lot, material batch, date, process route, inspection status and approved deviations. For projects with long service life or regulated requirements, component, firmware, serialization and chain-of-custody information may also matter.
IPC-1782 describes risk-based manufacturing and supply-chain traceability for electronic products. Its underlying lesson is practical: collect traceability that supports investigation and containment, rather than creating data with no defined use. During supplier evaluation, ask how quickly the supplier can identify other affected lots when one failure is found.
2.6 Change control
Many field problems are not caused by an incapable initial process but by an uncontrolled change after approval. The supplier-evaluation package should define which changes require notification or approval. Examples may include laminate or solder-mask substitutions, stackup changes, surface-finish chemistry, production location, external process source, key equipment, test method, panelization or acceptance criteria.
Ask for a realistic workflow: who identifies a proposed change, how technical impact is reviewed, what evidence supports approval, how the effective lot is recorded and how obsolete instructions are prevented from returning to production. “Same specification” does not always mean “same behavior” for impedance, assembly, reliability or appearance.
2.7 Nonconformance, containment and corrective action
A supplier is not qualified because it claims that defects never occur. It is qualified when it can detect, contain, communicate and correct problems in a controlled way. Evaluate the expected response to a nonconformance:
- How is the affected stock and work in progress identified and contained?
- How quickly is the customer informed when shipment or performance may be affected?
- Who has authority to approve deviation, rework, repair or scrap?
- How are root cause and escape cause separated?
- How is corrective action verified for effectiveness on later lots?
An 8D report is useful only when its evidence matches the actual failure mechanism. Generic statements such as “operator training strengthened” are not a substitute for a verified cause, process change and recurrence check.
2.8 Capacity, ownership and external-process transparency
A capability table often says little about who performs each process and whether capacity is available for the required lead time. Supplier evaluation should map responsibility for fabrication, assembly, special finishes, testing, component sourcing and logistics. Where qualified manufacturing partners are used, the customer still needs a clear owner for data control, approval, inspection, communication and nonconformance management.
This does not mean every process must be under one roof. It means the route must be transparent enough to control risk. ISO guidance on externally provided processes emphasizes that outsourcing does not remove the organization’s responsibility to ensure that requirements are met.
3. Use a sample or pilot order as a controlled qualification step
A pilot build should test the proposed production system, not merely produce a few visually acceptable boards. Before the order, define what the pilot must demonstrate and which records will be reviewed. The checklist may include:
- approved data revision and documented engineering questions;
- confirmed stackup, material, copper and surface finish;
- panel drawing or assembly array approval where applicable;
- required coupons, impedance or microsection plan;
- electrical test and inspection records;
- packaging, labelling and traceability fields;
- deviation and change-notification rules;
- delivery documentation and communication timing.
Do not scale immediately from a successful five-piece sample to a high-volume order without considering the change in panel utilization, tooling, cycle time, material lot, process loading and inspection sample size. A production-representative pilot is stronger evidence than a hand-selected engineering sample.
4. A practical PCB supplier-evaluation scorecard
| Evaluation area | Weak evidence | Stronger evidence |
|---|---|---|
| Technical capability | Marketing table only | Design-specific DFM, process route and limits confirmed |
| Quality system | Certificate image only | Relevant procedures, responsibilities and current records |
| Sample validation | Photos or unlinked samples | Records tied to revision, material, lot and acceptance criteria |
| Process control | Equipment list | Defined controls, calibration, reaction plan and evidence of use |
| Inspection and test | “100% inspection” statement | Method, coverage, limits, result status and failure handling |
| Traceability | Date code on packaging | Lot-to-material/process/inspection linkage appropriate to risk |
| Change control | Informal promise | Defined notification, approval, effective-lot and revision process |
| Corrective action | Generic 8D template | Containment, verified root cause, escape cause and effectiveness check |
| Capacity and continuity | Nominal monthly capacity | Lead-time assumptions, constraints, backup route and escalation owner |
| Communication | Fast quotation | Accurate engineering questions, decision records and accountable ownership |
The weighting should match product risk. A low-complexity prototype and a safety-critical, long-life assembly should not use the same approval threshold. Buyers should also separate “mandatory gate” items from scored preferences. For example, an unresolved material requirement or missing change-control agreement may be a stop condition even if the total score appears high.
5. Qualification is not the end of supplier control
Supplier performance must be reviewed using actual order data. Suitable indicators may include on-time delivery, first-pass acceptance, customer escapes, repeat defects, response time, corrective-action effectiveness, unauthorized changes and documentation accuracy. The trend matters more than a single perfect or imperfect lot.
Periodic review should also consider whether the product, volume, material availability, production location or regulatory context has changed. Requalification may be appropriate after a major process change, long production gap, repeated quality issue or transfer to a different manufacturing route.
A quality-management-system certificate can add confidence, but it does not replace product-specific evidence. Likewise, an audit is a point-in-time assessment, not a permanent guarantee. The most reliable supplier relationship combines clear requirements, transparent controls, objective records and disciplined communication throughout the product life cycle.
Technical references
- ISO 9001 Auditing Practices Group — Guidance on External Providers.
- IPC-1782 — Standard for Manufacturing and Supply Chain Traceability of Electronic Products.
- Global Electronics Association — IPC standards-related resources and digital data exchange.
- Global Electronics Association — Digital manufacturing and traceability resources.
Evaluating a PCB or PCBA supply route?
JEXPCB can coordinate design review, fabrication, assembly, component sourcing, project-specific testing and international delivery through qualified manufacturing resources. We focus supplier evaluation on the evidence required for the actual project rather than unsupported capability claims.