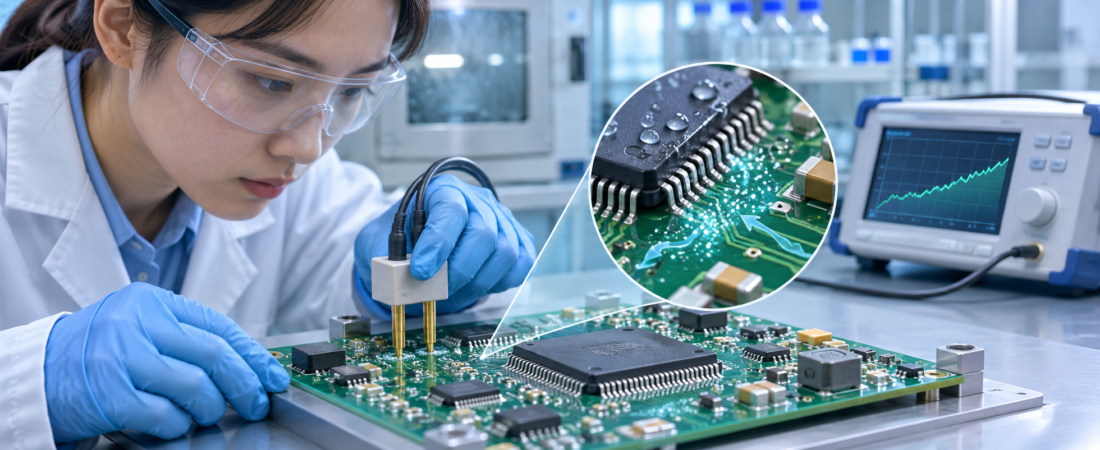
A PCBA can look perfectly clean and still carry reliability risk. Ionic residues are often invisible. When moisture is present and an electric field exists, mobile ions can increase leakage current, reduce insulation resistance, support electrochemical migration and contribute to corrosion. The result may be intermittent behavior, dendritic growth or a field failure that never appeared during normal visual inspection.
The correct question is not simply whether a board was washed. It is whether the complete assembly process leaves residues compatible with the product’s voltage, spacing, environment, coating strategy and required service life. That requires process knowledge and objective evidence—not a generic cleanliness number copied from another product.
1. Why ionic residue becomes an electrical problem
Flux activators, plating chemicals, handling contamination, wash chemistry and environmental deposits can leave ionic material on an assembly. In a dry state, the board may pass functional test. Under humidity or condensation, however, residue can dissolve into a conductive film. Bias then moves charged species between conductors.
| Risk factor | Why it changes the outcome | Questions for review |
|---|---|---|
| Residue chemistry | Different ionic species have different mobility, corrosiveness and response to extraction. | Which flux, cleaner, plating and handling materials contact the board? |
| Moisture exposure | Humidity or condensation can dissolve residue and create an electrolyte path. | What temperature, RH, condensation and storage conditions are credible? |
| Electrical bias and spacing | Higher field strength across fine spacing increases migration and leakage sensitivity. | Which high-impedance, high-voltage or fine-pitch nodes are exposed? |
| Residue location | Low-standoff components can trap active material and block cleaning or outgassing. | Can flux remain under QFN, BGA, shield cans or connectors? |
| Service life | Small leakage or corrosion mechanisms can accumulate over long exposure. | Is the product disposable, industrial, automotive, medical or long-life infrastructure? |
2. Identify contamination sources across the entire process
Do not limit the review to reflow. Bare-board fabrication can leave plating or etching residues. Solder paste, liquid flux, selective soldering, wave soldering, hand soldering and rework can each add chemistry. Fingerprints, gloves, fixtures, stencil-cleaning fluid, wash-water quality and poorly maintained cleaning equipment can also change the ionic load.
A process map should identify every chemical contact, thermal activation step, cleaning stage, rinse, drying step and manual handling point. Record material name and revision, supplier, process window, board family and any change that could invalidate earlier evidence. A flux classification alone does not prove that every assembly geometry will be reliable without cleaning.
3. Understand what common test methods can—and cannot—prove
IPC-TM-650 methods 2.3.25 and 2.3.26 describe solvent-extract conductivity approaches often associated with ROSE testing. These methods extract ionizable surface contamination and report an equivalent conductivity result. They are useful for process monitoring, but they do not identify each ion, show its exact location or reproduce every biased-humidity failure mechanism.
| Method | Useful evidence | Important limitation |
|---|---|---|
| ROSE / extract conductivity | Fast trend monitoring for total extractable ionic content under a controlled method. | Does not identify species or location; results depend on extraction, area calculation and equipment. |
| Ion chromatography | Identifies and quantifies selected ionic species, helping trace a residue to a process source. | Sampling and extraction still matter; a bulk result may hide local concentration. |
| SIR testing | Evaluates electrical insulation behavior under controlled temperature, humidity and bias. | Usually requires representative coupons or test vehicles and a defined test design. |
| Visual inspection | Finds visible residue, water marks, corrosion, coating defects and handling problems. | Cannot demonstrate absence of invisible ionic contamination. |
| Product reliability test | Shows performance of the actual design under defined environmental and electrical stress. | A weak sample plan or unrealistic stress can miss low-frequency mechanisms. |
4. Replace the universal limit mindset with process-specific evidence
Current assembly practice increasingly emphasizes objective evidence. A historical generic ROSE limit should not be treated as automatic proof that every no-clean or cleaned process is acceptable. The manufacturer and customer should define the product classes, materials, assembly geometries, environmental conditions, sampling plan, test method and acceptance criteria that support the decision.
Start with the highest-risk board family rather than the easiest coupon. Include the tightest spacing, lowest standoff, most difficult-to-clean regions, maximum flux exposure and relevant rework sequence. Establish a qualified baseline, then use production monitoring to detect drift. When material, equipment, wash chemistry, supplier, layout or coating changes, decide whether the evidence remains valid.
5. Cleaning is a controlled process, not a cosmetic operation
If cleaning is required, match the chemistry and equipment to the flux and component set. Control wash concentration, temperature, spray pressure, time, rinse-water quality, bath loading, filtration and drying. A poor cleaning process can redistribute residue under low-standoff packages or leave conductive rinse contamination.
Confirm component compatibility before immersion or aggressive cleaning. Open switches, microphones, relays, sensors, displays, unsealed transformers and labels may need protection or a different process. Verify drying, because trapped moisture can undermine both electrical testing and conformal coating adhesion.
6. Conformal coating does not erase contamination
Coating over active residue can trap contamination and moisture against the board. It may also create adhesion loss, bubbles or pathways at component edges. Cleanliness requirements should therefore be defined before coating, together with masking, cure and inspection controls. If a no-clean residue is intentionally left under coating, qualification evidence should cover that exact material and process combination.
7. Build cleanliness control into production release
| Control point | What to define | Release evidence |
|---|---|---|
| Materials | Approved paste, flux, cleaner, rinse and coating revisions. | Lot traceability and controlled change record. |
| Process window | Flux application, thermal profile, wash and drying parameters. | Recorded parameters and maintenance status. |
| Sampling | Board families, frequency, sample timing and escalation rules. | Approved sampling plan and trend history. |
| Test method | Extraction, area calculation, equipment, limits and correlation to reliability. | Method revision, calibration and test report. |
| Nonconformance | Containment, retest, root cause and disposition authority. | Documented lot disposition and corrective action. |
8. A practical JEXPCB cleanliness-review workflow
Provide the controlled BOM, PCB finish, assembly drawing, product class, operating voltage, minimum conductor spacing, environment, flux and solder-paste data, cleaning requirements, conformal-coating specification and any customer cleanliness limits. Identify low-standoff packages, high-impedance nodes and previous contamination failures.
JEXPCB can coordinate process review, representative sample builds, cleanliness testing and project-specific inspection through its PCBA manufacturing network and qualified laboratory partners. The test method, sampling plan and acceptance criteria should be approved before production release. Submit the controlled package through the PCBA quotation page.
Frequently asked questions
Does a no-clean flux mean the PCBA never needs cleaning?
No. “No-clean” describes a flux classification and intended residue behavior under qualified conditions. Board geometry, flux volume, thermal activation, environment, coating and reliability requirements can still justify cleaning or additional validation.
Can ROSE testing identify the contaminating chemical?
No. It measures the conductivity response of extracted ionizable material and reports a combined result. Ion chromatography is more suitable when specific ionic species must be identified.
Can a board pass functional test and still fail later?
Yes. A dry board can function normally while ionic residue remains. Humidity, condensation and bias during service can activate leakage, corrosion or electrochemical migration mechanisms.
Should every production lot receive the same test?
Not automatically. The sampling plan should follow product risk, process capability, change history and customer requirements. Higher-risk or unstable processes need stronger monitoring and escalation rules.
Technical references
- Global Electronics Association — IPC J-STD-001J overview
- IPC-TM-650 Method 2.3.26 — Ionizable Detection of Surface Contaminants
- Global Electronics Association — Test methods for flux and process residues
- IPC educational material — Objective evidence and ionic process monitoring
Technical references checked 5 November 2026.