
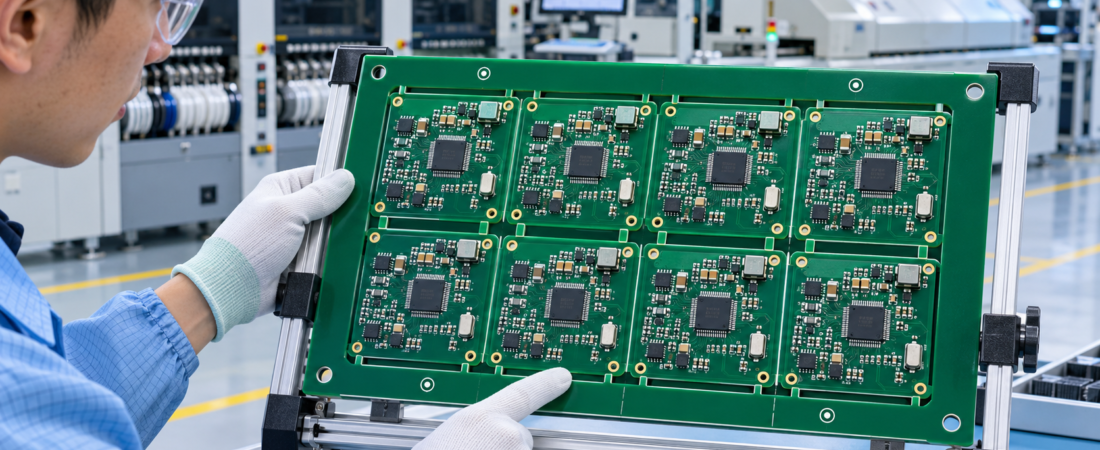
A good PCBA panel is not only a way to fit more boards into one manufacturing sheet. It is a temporary mechanical platform that must survive solder-paste printing, component placement, reflow, inspection, testing, handling and depanelization without losing registration or damaging the product.
Panel rails, fiducials, tooling holes, breakaway tabs and V-scores should be designed as one system. If they are added after the PCB layout is complete, the result may be unstable conveyance, poor stencil support, inaccessible inspection areas, component stress or excessive manual work.
1. Start with the complete manufacturing flow
Ask how the panel will enter and leave every machine. Stencil printers need stable support and sufficient edge access. Pick-and-place equipment needs reliable fiducials and a repeatable conveyor datum. Reflow, AOI, X-ray and test fixtures may impose different clearance, orientation and support requirements. Depanelization introduces its own stress and tool-access constraints.
| Process | Panel design need | Typical failure if missed |
|---|---|---|
| Stencil printing | Flat support, suitable rail width and access for board supports and clamps. | Paste variation, panel movement or unsupported thin areas. |
| Placement | Global fiducials, consistent datum, component keepout and conveyor clearance. | Rotational offset, local placement error or rail collision. |
| Reflow | Balanced layout, sufficient stiffness and controlled copper/thermal distribution. | Panel sag, bow, twist or uneven heating. |
| AOI / X-ray / test | Readable board identity, optical access and fixture access to test points. | Wrong traceability, blocked inspection or unusable fixture probes. |
| Depanelization | Tool path, component clearance, supported breakaway and acceptable edge finish. | Cracked MLCCs, laminate damage, burrs or board flexure. |
2. Define rail function before rail width
Rails create a straight, repeatable transport edge when the product outline is small, irregular or crowded with edge components. They also provide space for global fiducials, tooling holes, coupons, barcodes and handling areas. The correct width depends on printer clamps, conveyor belts, edge-clearance rules and any wave or selective-solder pallet.
Specify which rails are process rails and whether they are removed before shipment. Keep copper, components and fragile overhangs away from clamp, conveyor and depanelization zones. If rails are only needed on two sides, confirm that panel stiffness and machine support remain adequate.
3. Use fiducials as an optical coordinate system
Global fiducials allow the placement system to correct translation, rotation and scale for the panel. Local fiducials may be needed for fine-pitch or high-risk component groups, depending on equipment capability and product requirements. The mark, solder-mask clearance, surface finish and surrounding contrast should be consistent and readable.
Place global marks far enough apart to create a stable coordinate reference and avoid a symmetrical pattern that can permit incorrect orientation. Do not crowd them with silkscreen, copper graphics, tooling hardware or board edges. Confirm the exact fiducial geometry with the assembler rather than applying a generic dimension without equipment context.
4. Separate tooling holes from product mounting holes
Tooling holes locate the panel on printers, fixtures, pallets or depanelization equipment. Their diameter, tolerance, plating status and position should be clearly defined. Use a non-symmetrical pattern where orientation control is required. Keep them in mechanically stable rail regions and away from slots or break lines that can weaken the datum.
A product mounting hole is not automatically a suitable process datum. If the same feature is reused, confirm positional tolerance, plating, wear, fixture pin type and the stage at which rails are removed. Record the datum scheme on the fabrication and assembly drawing.
5. Choose the breakaway method from product geometry and risk
| Method | Where it can fit | Main controls |
|---|---|---|
| V-score | Straight separation lines and compatible board outlines; efficient for regular arrays. | Remaining web, copper/component keepout, board thickness, grain direction and controlled depaneling equipment. |
| Tab routing with mouse bites | Irregular outlines, mixed shapes or locations that cannot use a continuous score. | Tab position/width, perforation pattern, router access, edge finish and residual nib removal. |
| Solid tab + router depaneling | Products needing low mechanical stress or a cleaner controlled edge. | Fixture support, cutter path, dust extraction and component clearance. |
| Laser depaneling | Thin, small or stress-sensitive boards where the approved material/process is suitable. | Heat-affected zone, carbonization, fumes, cycle time and material qualification. |
Manual snapping is simple but can generate high board strain. It is especially risky near MLCCs, BGAs, brittle components, solder joints and connectors close to the break line. Where reliability matters, define and validate the actual depanelization tool and support method.
6. Place tabs where they support the panel without harming the product
Tabs should keep each circuit secure through printing, placement and reflow while allowing predictable separation. Distribute them to resist rotation and sag. Avoid placing a tab beside an MLCC, BGA corner, fine-pitch connector, sensitive solder joint or weak laminate area. Consider how the residual nib will be removed and whether the finished edge has a dimensional or cosmetic requirement.
Do not cut through copper, controlled-impedance structures or critical return paths unless explicitly designed and reviewed. Keep routed slots and cutouts from creating narrow panel ligaments that can fracture during handling.
7. Control orientation, traceability and mixed variants
A panel can contain identical units, rotated units or product variants. Rotation may improve utilization, but it can complicate polarized placement, wave soldering, thermal balance, inspection programs and operator handling. Mixed panels require clear unit identity, BOM mapping, program control and traceability.
Use an unambiguous pin-one/orientation scheme and a controlled board identifier. Confirm whether the serialization occurs at panel level, unit level or both, and whether the code remains readable after depanelization.
8. Release a complete panel package
| Package item | What it should show | Why it matters |
|---|---|---|
| Panel drawing | Overall size, array, rails, spacing, orientation and unit references. | Creates one mechanical definition for fabrication and assembly. |
| Breakaway detail | V-score, route, tab, mouse-bite and finished-edge requirements. | Prevents the CAM operator from choosing an unsuitable separation method. |
| Datum features | Fiducial and tooling-hole size, location, clearance and tolerance. | Aligns optical and mechanical coordinate systems. |
| Keepouts | Conveyor, clamp, pallet, router and component restrictions. | Protects parts and maintains equipment access. |
| Assembly data | Panel coordinates, centroid origin, variants, barcode and test mapping. | Prevents program and unit-identity mismatches. |
9. A practical JEXPCB panel-review workflow
Send the single-board Gerber or ODB++ package, board outline, stack-up, BOM, centroid, assembly drawings, component height map, test-point file, expected assembly process and required finished-edge condition. Identify any customer-defined panel size, stencil, pallet, fixture or depanelization constraint.
JEXPCB can coordinate fabrication CAM review and PCBA process review so panel utilization, SMT stability and separation risk are evaluated together through its manufacturing network and qualified partners. Final panel dimensions and feature rules should be confirmed against the selected line and project tooling before release. Submit the package through the PCBA quotation page.
Frequently asked questions
Should customers always design the production panel?
No. A customer-defined panel can be useful when it must match existing tooling, but the selected fabricator and assembler should review it. For a new product, supplying a controlled single-board dataset and process constraints often allows the manufacturing team to propose a more suitable panel.
Is V-scoring always cheaper than tab routing?
Not always. V-score can be efficient for straight regular arrays, but geometry, component clearance, board thickness, stress and finished-edge requirements may favor routing or another method.
Do all components need local fiducials?
No. Need depends on package pitch, placement equipment, board stability and process capability. Global panel fiducials are fundamental; local fiducials should be added when the risk and equipment strategy justify them.
Can multiple PCB variants share one panel?
Yes, but BOM, placement, traceability, yield and scheduling must be controlled. A mixed panel can reduce flexibility if one variant is delayed or has a different process requirement.
Technical references
- Eurocircuits — Customer Panel Basics
- Eurocircuits — Customer Panel by Eurocircuits
- Eurocircuits — Fiducials
- Eurocircuits — How to Panelise Small PCBs
Technical references checked 5 November 2026. Exact panel dimensions and equipment rules remain supplier- and project-specific.