

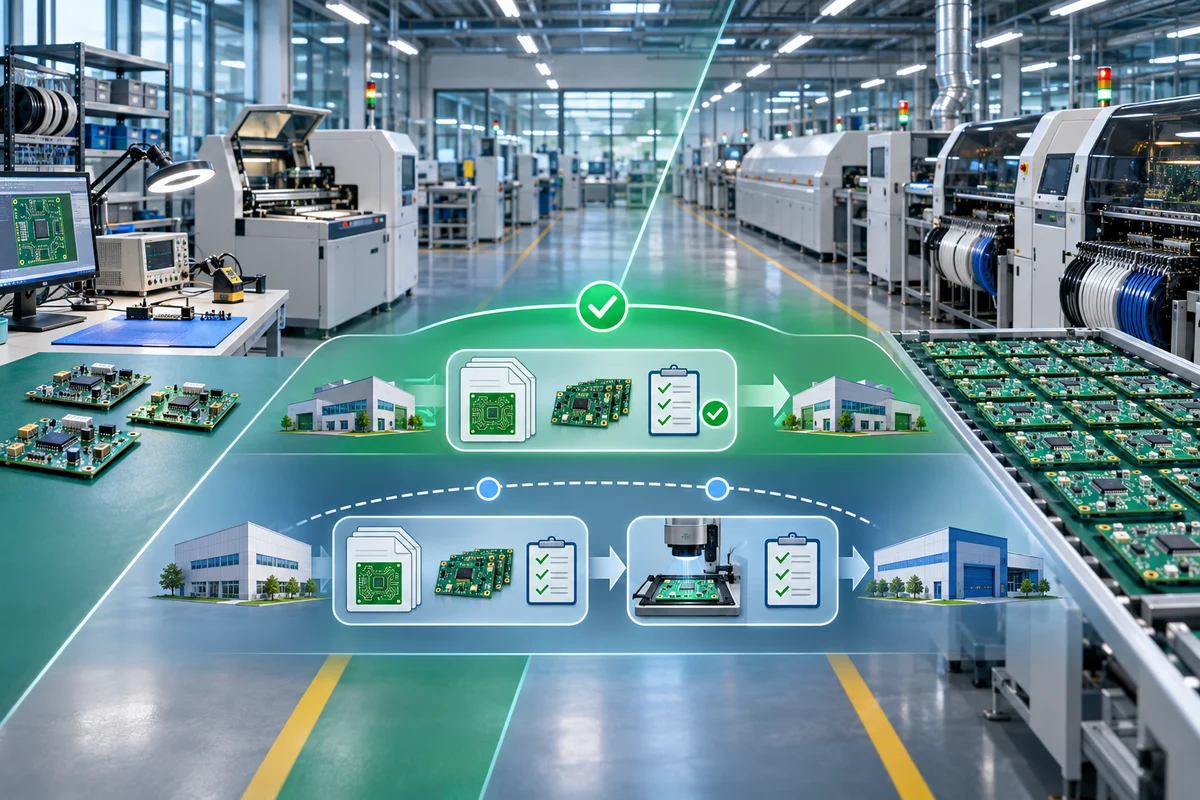
Using one supplier from prototype through mass production preserves process knowledge and reduces transfer effort. But a fast prototype shop may not have the equipment, certifications, capacity, automation or cost structure needed for stable volume.
The right answer is therefore not always “same supplier” or “different supplier.” It is a planned sourcing model with clear data ownership, qualification gates and contingency capacity.
1. Compare the jobs the supplier must perform
Prototype work rewards quick engineering response and flexible change handling. Volume rewards repeatability, capacity planning, automation, change control and supply continuity.
| Requirement | Prototype priority | Volume priority |
|---|---|---|
| Lead time | Fast material and engineering loop | Predictable takt and capacity. |
| Change handling | Frequent revision and feedback | Formal ECO and configuration control. |
| Process | Flexible routing and manual intervention | Stable automated process and SPC. |
| Commercial model | Low quantity and setup tolerance | Yield, panel efficiency and total landed cost. |
2. Keep one supplier when learning must carry forward
One supplier is attractive when the technology is specialized, the production site is already volume-capable, or process tuning and test fixtures are difficult to transfer.
| Signal | Why one supplier helps | Condition |
|---|---|---|
| Special materials/process | Retains qualified stack-up and recipes | Supplier has proven volume capacity. |
| Fast ramp | Avoids repeating DFM and FAI | Revision control is disciplined. |
| Complex PCBA | Carries stencil, profile and test learning | Assets and records are customer-accessible. |
| Regulated product | Reduces requalification events | Quality system covers production scope. |
3. Split or dual-source when risk demands it
A separate volume supplier can improve economics and capacity, but only through a controlled transfer package and pilot qualification.
| Transfer item | Minimum content | Gate |
|---|---|---|
| Product data | Gerber/ODB++, BOM, CPL, drawings and approved deviations | Independent data review. |
| Process evidence | Stack-up, coupons, profiles, stencil and inspection programmes | Pilot/FAI approval. |
| Quality plan | CTQ, sampling, traceability and change control | Capability and audit evidence. |
| Supply plan | Materials, capacity, forecast and recovery route | Ramp readiness. |
Choose the model before design freeze
A practical approach is to qualify the intended volume supplier during a late prototype or engineering-validation build. Keep a rapid prototype source for learning, but transfer controlled files, approved deviations and inspection evidence. For critical products, establish a second source before a disruption—not during one.
Frequently asked questions
Is the same supplier always cheaper?
No. Transfer costs may be lower, but the supplier’s volume yield, panel utilization and capacity determine recurring cost.
When should the volume supplier enter?
Before design freeze or during validation, while changes are still manageable.
Can prototype quality predict volume quality?
Only partly. A few manually supported boards do not prove volume process capability.
Management references
- ISO 9001 — Quality management systems
- Global Electronics Association — IPC standards
- NIST MEP — Supplier scouting resources
References checked 15 November 2026. Supplier strategy should be based on product risk, audited capability and contracted change control.